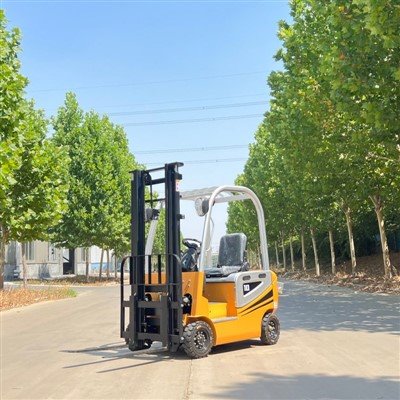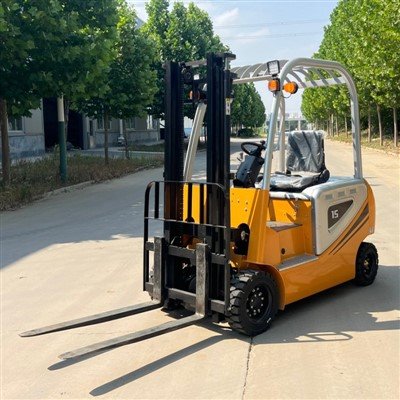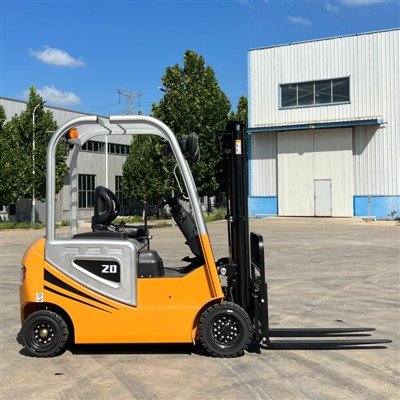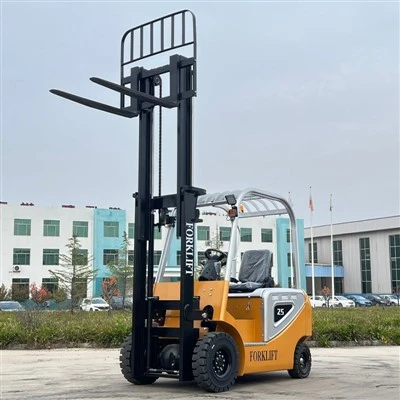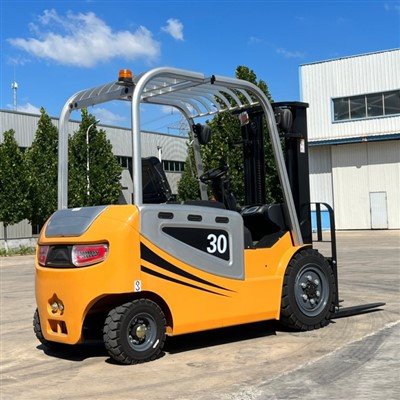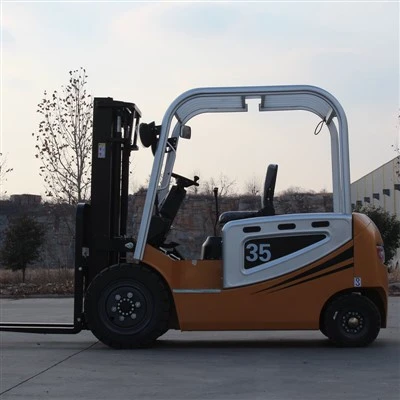
Our engineering team frequently supports food processing and pharmaceutical facilities facing material handling challenges. Many cold-chain food plants struggle with HACCP(Hazard Analysis and Critical Control Points) audit risks caused by diesel forklift exhaust contamination. Electric forklifts often face performance issues in low-temperature environments, leading to costly downtime during multi-shift operations.
A common question from facility managers is: "Which LPG forklift can keep our operations running while maintaining compliance?"
With more than 10 years of experience in material-handling solutions for food processing, pharmaceutical warehouses and cold-chain applications, our engineering team has resolved these challenges across numerous projects.
LPG forklifts provide lower-emission indoor operation compared with diesel forklifts, strong runtime performance and heavy-duty capability. However, incorrect specification of capacity, mast height or working conditions can lead to reliability and compliance issues.
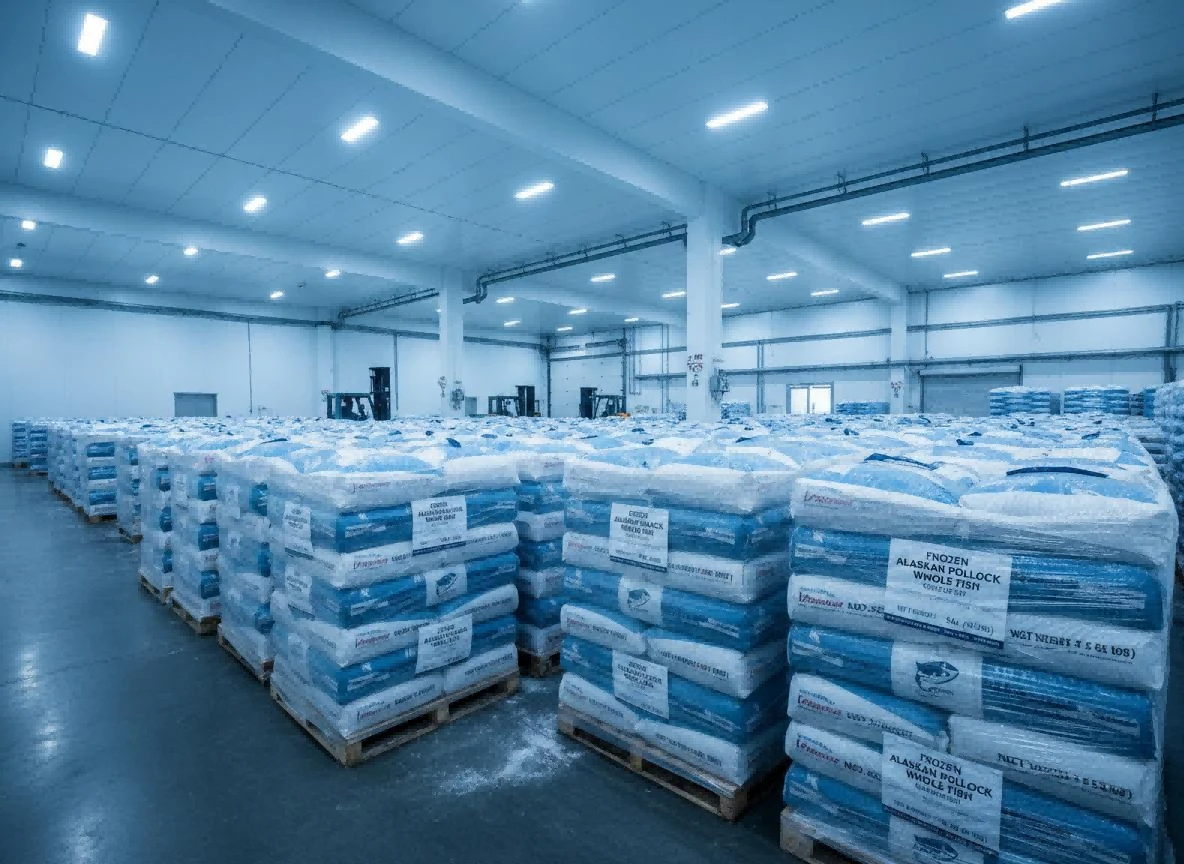
Our engineering team supported a large frozen-food processing facility in North America.
The site spans 8,000 m², including production areas, cold-chain logistics zones and outdoor loading docks. The plant operates two 8-hour shifts daily, totaling 16 hours of operation. Materials handled include frozen seafood, meat blocks and packaged meals, with typical loads from 1.5 ton to 2.2 ton.
Common on-site challenges included:Diesel forklifts caused soot contamination, risking failed food safety audits;Electric forklifts experienced reduced performance in low-temperature areas;Narrow 3.5-metre aisles required compact turning radius;Mixed indoor-outdoor operation demanded high flexibility
After evaluating working conditions, our team identified key requirements: low-emission operation, stable multi-shift performance, compact design and sufficient capacity for peak loads.
Our recommendation was a 2.5-ton LPG forklift with a 4500 mm triplex mast and application-specific modifications.
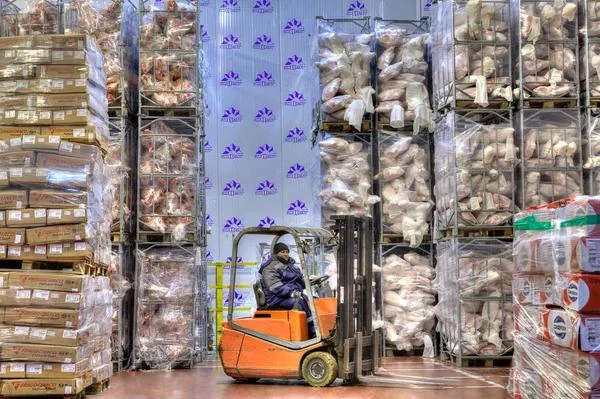
Key specificationsRated capacity: 2.5 ton (500mm load center);Fuel type: LPG (low particulate emissions suitable for food-grade areas);Mast height: 4500 mm;Turning radius: 2200 mm;Runtime: Approximately 8 hours per LPG cylinder; quick cylinder change supports continuous operation
Additional enhancements included food-grade hydraulic fluid and enclosed exhaust components to reduce fume exposure.After implementation, the customer achieved:Successful food-safety audit results;Significantly reduced unplanned downtime;Stable performance in cold-chain logistics and loading areas
For mixed indoor-outdoor operations around cold storage facilities, LPG forklifts provide clear advantages in runtime flexibility. For dedicated deep-freeze rooms below -18°C, special cold-weather configurations are required to ensure engine startup, sealing and lubrication perform reliably.
Our engineering team also supported a pharmaceutical distribution center in Europe.
The facility stores medicines, vaccines and medical consumables, operating under strict EU GMP standards for indoor air quality and cleanliness.
Key challenges:Zero tolerance for contamination or exhaust emissions;24-hour three-shift operation;High stability requirements for valuable pharmaceutical goods;Clean, easy-to-clean equipment surfaces
The 6,500 m² warehouse includes temperature-controlled zones (15–25°C) and narrow aisles. Most loads range from 1 ton to 1.5 ton.
Previously used electric forklifts required large charging rooms and frequent battery changes. Diesel equipment was prohibited indoors due to emission risks.
Our engineering team focused on three priorities: low-emission operation, continuous multi-shift performance and stable, low-vibration lifting.
The recommended solution was a custom 1.5-ton LPG forklift designed for pharmaceutical environments
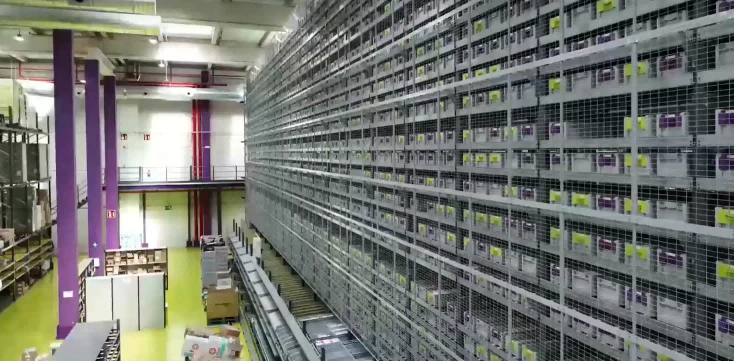
Key specifications:Rated capacity: 1.5 ton (500mm load center);Fuel type: LPG for low-emission indoor operation;Mast height: 3000–5000 mm;Features: Reinforced mast, anti-vibration tires, smooth hydraulics;Design: Sealed electric parts, dust-proof chassis for easy cleaning
As an experienced LPG forklift manufacturer, we provided OEM customization including: stainless steel forks, low-noise engine design (<65dB) and leak-proof LPG fuel systems.
After deployment, the customer achieved:Full compliance with GMP requirements;Stable 24/7 operation;Zero contamination incidents
;Improved workflow efficiency
How to Choose the Right LPG Forklift for Different Applications
Based on hundreds of food and pharmaceutical projects, our engineering team uses a clear, practical selection framework.
Match capacity to your actual pallet weights:1.0ton LPG forklift: Light-duty operations, pharmaceutical carton handling, packaging lines;1.5ton LPG forklift: Most food warehouses and pharmaceutical distribution centers;2.5ton LPG forklift: Heavy-duty food processing, cold-chain logistics, outdoor loading
Spec for your operating environment:Food processing warehouse: Easy-clean surfaces, enclosed exhaust, food-grade fluids;Pharmaceutical warehouse: GMP compliance, low-emission, low-vibration, easy-sanitize design;Outdoor / loading docks: Durable tires, weather-sealed components, stable performance
LPG Forklift vs Electric Forklift
A common comparison for food and pharma buyers is LPG vs electric forklifts.
Advantages of LPG ForkliftsUltra-fast refueling: 2-minute cylinder swap;Stable performance in varying temperatures;No voltage drop under heavy loads;No charging room or extra battery cost
Limitations of LPG Forklifts:Requires proper indoor ventilation;Needs safe LPG cylinder storage;Not zero-emission
Electric forklifts remain suitable for single-shift, fully enclosed clean rooms. For multi-shift, mixed indoor-outdoor or cold-chain environments, the LPG forklift is often the more practical warehouse forklift solution.
Key Factors Before Buying an LPG Forklift
1.Daily operating hours
2.Indoor ventilation conditions
3.Actual peak load weight
4.Aisle width and mast height
5.Industry compliance (HACCP, GMP)
Work with an experienced LPG forklift manufacturer that understands food and pharmaceutical requirements.
Why Choose Our LPG Forklift Solution
With more than 10 years supporting global food and pharmaceutical projects, our team provides customized warehouse forklift solutions.
Our advantages:Application-specific LPG forklift design;Flexible OEM customization;Full capacity range: 1.0T / 1.5T / 2.5T;Global after-sales support;Compliance-focused engineering
We evaluate real site conditions before making recommendations. Contact our engineering team for a no-obligation assessment.
Choosing the right LPG forklift for food processing and pharmaceutical warehouses depends on capacity, environment, compliance and operating shifts.
1.0-ton: Light pharma & packaging
1.5-ton: Standard food & pharma warehousing
2.5-ton: Heavy food processing & cold chain
LPG forklifts provide lower-emission indoor operation compared with diesel forklifts and strong multi-shift performance. For cold-chain facilities, they excel in mixed indoor-outdoor logistics areas; deep-freeze applications require cold-weather configuration.
As a trusted LPG forklift manufacturer, we help you reduce audit risks and downtime with properly specified material handling equipment.
If you need support selecting the right LPG forklift for your facility, contact our engineering team for a free consultation